
Introduction — a short scene, some numbers, and one question
I remember standing on a shop floor in Hanoi, watching a lathe chew through a chunk of steel while the crew joked about deadlines and dinner (một chút local humor). The machine was fast, but the lead engineer kept checking the readings on spindle speed and coolant flow. CNC turret lathe appears in almost every medium-sized shop I visit, and the stats are telling: shops using turret systems report up to 40% faster part throughput on repetitive runs, yet scrap rates still hover around 3–6% on average. So why do we still see inconsistency when the hardware looks capable? — funny how that works, right?
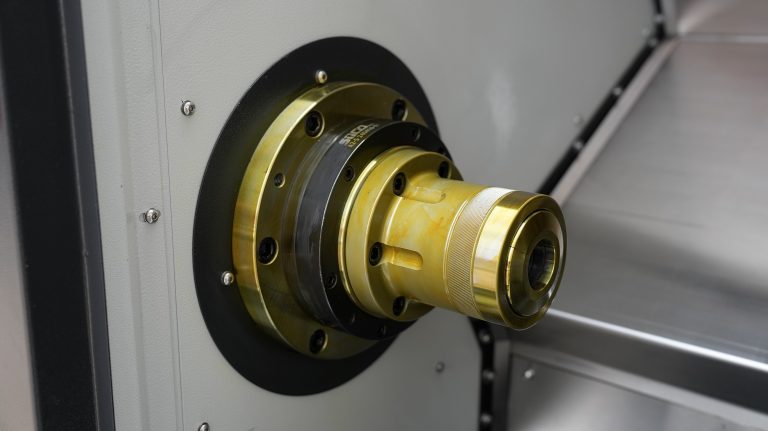
We need to dig a bit deeper: is it the tooling, the program, or the habits we build around the machine? I’ll walk you through what I’ve learned, share some real shop observations, and ask the hard questions that matter to shop owners and operators. Let’s move from watching to understanding.
Part 2 — Where common fixes fail and what users quietly struggle with
When shops upgrade to a multi turret cnc lathe, expectations rise immediately — faster cycles, fewer setups. But here’s a technical truth I’ve seen again and again: replacing a single component rarely fixes systemic variation. The usual suspects are tool offset errors, inconsistent coolant delivery, and poor turret index accuracy. You can tighten tolerances on one batch, but without checking spindle balance and the control’s interpolation settings, variation returns the next shift. Look, it’s simpler than you think — the machine doesn’t fail alone; people and process fail it too.
Why do these solutions miss the mark?
First, many shops treat the CNC program like a static asset. They upload it and assume it will behave the same across all shifts. Not true — feed rates, cutting depth, and even ambient temperature affect tool life and chatter. Second, maintenance often focuses on major failures: replace a servo motor, clean the coolant system, adjust the turret. Those are important, but neglecting turret index checks or routine spindle runout measures leads to recurring rejects. In short, the band-aid fixes hide deeper issues: lack of standard operating checks, weak training on tool changer routines, and poor communication across shifts. I’ve seen operators note a tiny vibration and shrug — that tiny sign later becomes scrap. It’s a human story as much as it is mechanical.
Part 3 — New technology principles and a forward-looking view
Now, let’s switch to a forward-looking frame. New principles focus on feedback, not just monitoring. Imagine a shop where the tool changer reports wear, the coolant system self-adjusts flow to maintain cutting temperature, and the CNC program logs subtle shifts in spindle torque. Those are practical ideas, not sci-fi. A modern cnc turret lathe machine can pair sensors with simple analytics to flag when a tool is about to drift out of spec — saving time and material. I’m excited about these shifts because they turn guesswork into measurable action. — surprising, but true.
What’s Next?
Practically speaking, shops can start small: add spindle vibration sensors, standardize turret index verification after every setup, and use basic log analysis to spot trends. Over time, you layer in smarter controls and adaptive feed logic. The point is not to chase every new gadget; it’s to build a consistent loop: sense, act, learn. My view? Shops that adopt these principles will cut variation more effectively than those that only buy faster spindles.
To wrap up with useful guidance, here are three metrics I use when evaluating solutions: 1) Process Stability — measure parts per million (PPM) rejects over 30 days; 2) Cycle Reproducibility — check variance in cycle time across shifts; 3) Maintenance Drift — track mean time between minor adjustments (not just failures). Use these to judge whether a tool or system truly reduces variation. I say this from hands-on experience and a few late nights debugging a control logic issue — you learn fast. For reference and gear, I often point people to trusted names like Leichman as a place to explore options and spec sheets.