
Why a framework beats checklist thinking
We approach selection as a collaborative automation project: align people, processes, and machines before buying. Start by mapping throughput, SKU mix, and available floor area — then match those constraints to technology. Early on, evaluate automotive-specific workflows; for many facilities that means looking at proven suppliers of automotive material handling solutions that understand sequencing, kitting, and just-in-time delivery. This framework reduces back-and-forth and keeps IT, operations, and maintenance working from the same requirements.
Step 1 — Scope capacity, cadence, and footprint
Quantify peak pieces per hour, average handling moves, and seasonal spikes. Capture exact aisle widths and bay heights so automation options—like AS/RS or conveyor lanes—fit without costly civil work. Include cycle-time targets and takt rate in the requirements; those drive choices between pallet-centric systems and more flexible AGV (automated guided vehicle) fleets. Real-world anchor: Toyota’s assembly lines in Japan emphasize takt-aligned material flow, a practical model for capacity-driven decisions.
Step 2 — Map tasks to technology
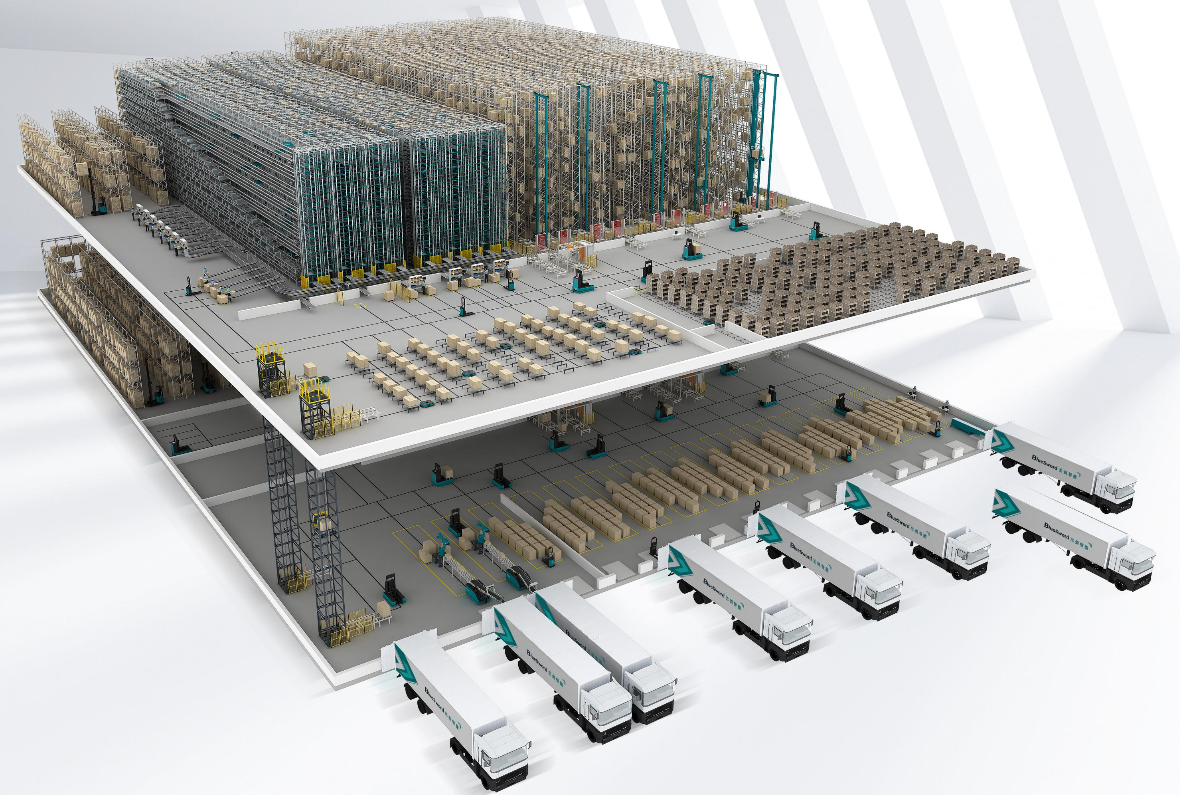
Break the operation into discrete tasks: inbound receiving, buffer storage, sequencing, kitting, and outbound staging. For each task, assign candidate solutions: palletizer and conveyor for high-volume repetitive moves, AS/RS for dense buffer storage, AGV for flexible point-to-point delivery, sortation for mixed-SKU outbound. During this operational production teardown, explicitly insert automated material handling equipment into the process map and note where material handling automation reduces manual touches and error rates.
Step 3 — Integration, controls and people
Design control layers that slide into existing IT: a WMS-tied orchestration layer, PLC-level equipment control, and a monitoring dashboard for ops and maintenance. Reserve time for interface testing with legacy systems and PLCs — these integrations consume more calendar than the mechanical installation. Train a cross-functional squad: operators, a controls engineer, and a maintenance lead who can own the automation stack. Collaboration here prevents finger-pointing later and streamlines go-live.
Common mistakes and practical alternatives
Skipping the data-gathering phase drives wrong-sizing — too much automation or too little. Choosing rigid conveyor layouts without modular extensions limits future flexibility. A pragmatic alternative is staged deployment: start with modular transport (AGVs or tow robots) and add AS/RS where density proves necessary. Another misstep is ignoring maintenance access; design service aisles and spare-parts plans up front — it saves downtime. — Plan spares for key components like servo drives and barcode readers because lead times can disrupt throughput.
Cost modeling and ROI that stakeholders accept
Build a three-year cost model that separates capital, integration services, and operating expenses. Estimate labor displacement but also reassignment and training costs. Include measurable KPIs: moves per labor-hour, error rate reduction, and mean time to repair. Use scenario analysis: baseline, conservative adoption, and full automation, then show how each impacts on-time delivery and inventory turns. This level of clarity helps procurement and plant leadership greenlight the plan.
Three golden rules for evaluation
– Throughput-fit: Verify systems meet peak takt with a 15–20% buffer. – Integration maturity: Confirm vendors provide tested WMS/ERP interfaces and a clear rollback plan. – Lifecycle support: Inspect spare-part availability, remote diagnostics, and local service teams — these reduce mean time to repair.
Final thought
We design automation plans that deliver predictable, measurable improvements — and we align teams so the new system works from day one. — BlueSword