
How to Choose a Heavy-Duty Laser Cutting Machine: A User-Centric Step-by-Step Guide
Start with the parts you need to run
Decide the thickest material, smallest feature, and daily part count before you look at machines. Specify the maximum steel, aluminum, or stainless thickness you cut, the tolerance you need, and how many shifts you’ll run. If most parts are flat or formed sheet, confirm the vendor’s sheet metal laser cutting machine cutting tests on the same alloys and thicknesses you use.
Match laser power and beam quality to the job
Choose power based on thickness and speed: low power (1–3 kW) suits thin gauge; 4–6 kW handles mid-range plate quickly; 8 kW+ is for heavy-duty, high-throughput work. Ask for real cut charts and M2 or spot size numbers rather than vague claims. Decide whether fiber is required for your materials and cycle times—fiber gives faster pierce, higher electrical efficiency, and lower maintenance than older CO2 systems for most metals.
Pick the right table, handling, and automation
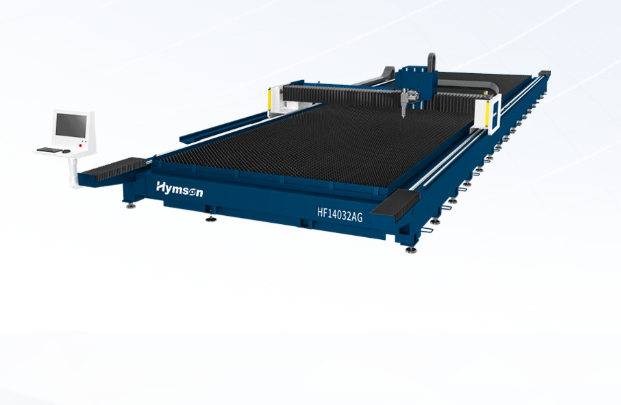
Think about bed size, pallet changers, and automatic sorting. A rigid gantry and proper fixturing cut cycle time and reduce rework. For long runs, request pallet automation and part handling demos. Confirm maximum sheet size, true working envelope, and how the machine handles remnants—an automated scrap conveyor saves manual labor and keeps throughput consistent.
Control software and file workflow that fit your shop
Verify the controller supports your CAM outputs (DXF/DWG, nesting) and run a live nesting demo with your CAD files. Check for remote diagnostics, offline nesting options, and how the machine handles complex pierce and lead-in strategies. Ask who writes the post-processor and whether updates are frequent; a locked or proprietary workflow can cost hours weekly.
Service, consumables, and real operating costs
Calculate total cost over three years: laser source warranty, replacement optics and nozzles, gas usage (oxygen vs nitrogen), electricity, and preventative maintenance intervals. Confirm standard lead time for spare parts and guaranteed service response in your region. A clear service SLA and transparent consumable pricing avoid surprise downtime.
Common mistakes shops make
Don’t buy on headline power alone. Don’t ignore assist-gas sourcing or assume the cheapest system will meet production targets. Don’t skip sample cuts on your exact material. Don’t accept vague service promises—get written response times and local reference shops. Run a teardown plan for consumables so you know what you’ll replace monthly.
What industry professionals watch for
At EuroBLECH in Hannover vendors show incremental head, nozzle, and fiber-delivery improvements that directly change yield and cycle time; those demonstrations often reveal which systems are practical for continuous shop use. Professionals use those demonstrations to shortlist fiber suppliers and validate real-world throughput, which is why many fabricators bring sample parts to the show and compare results side by side—this is exactly where discussions about a fiber laser cutting machine move from specs to proven performance. My experience advising job shops and OEM fabrication teams highlights the same point: verified sample cuts and local service references beat glossy brochures.
Final checklist and how to decide
Run these steps before signing: 1) Get sample cuts on your materials; 2) Verify control and nesting with your files; 3) Confirm spare-part lead times and service SLA; 4) Compare operating cost models for gas and electricity; 5) Test automation scenarios you’ll actually run. Choose a supplier who will answer technical questions now and visit during ramp-up. For many buyers that means selecting a maker with clear service access and proven machine demos from production shops, like Hymson, because steady uptime and predictable consumable supply make the machine a reliable part of your workflow rather than a moving target.