
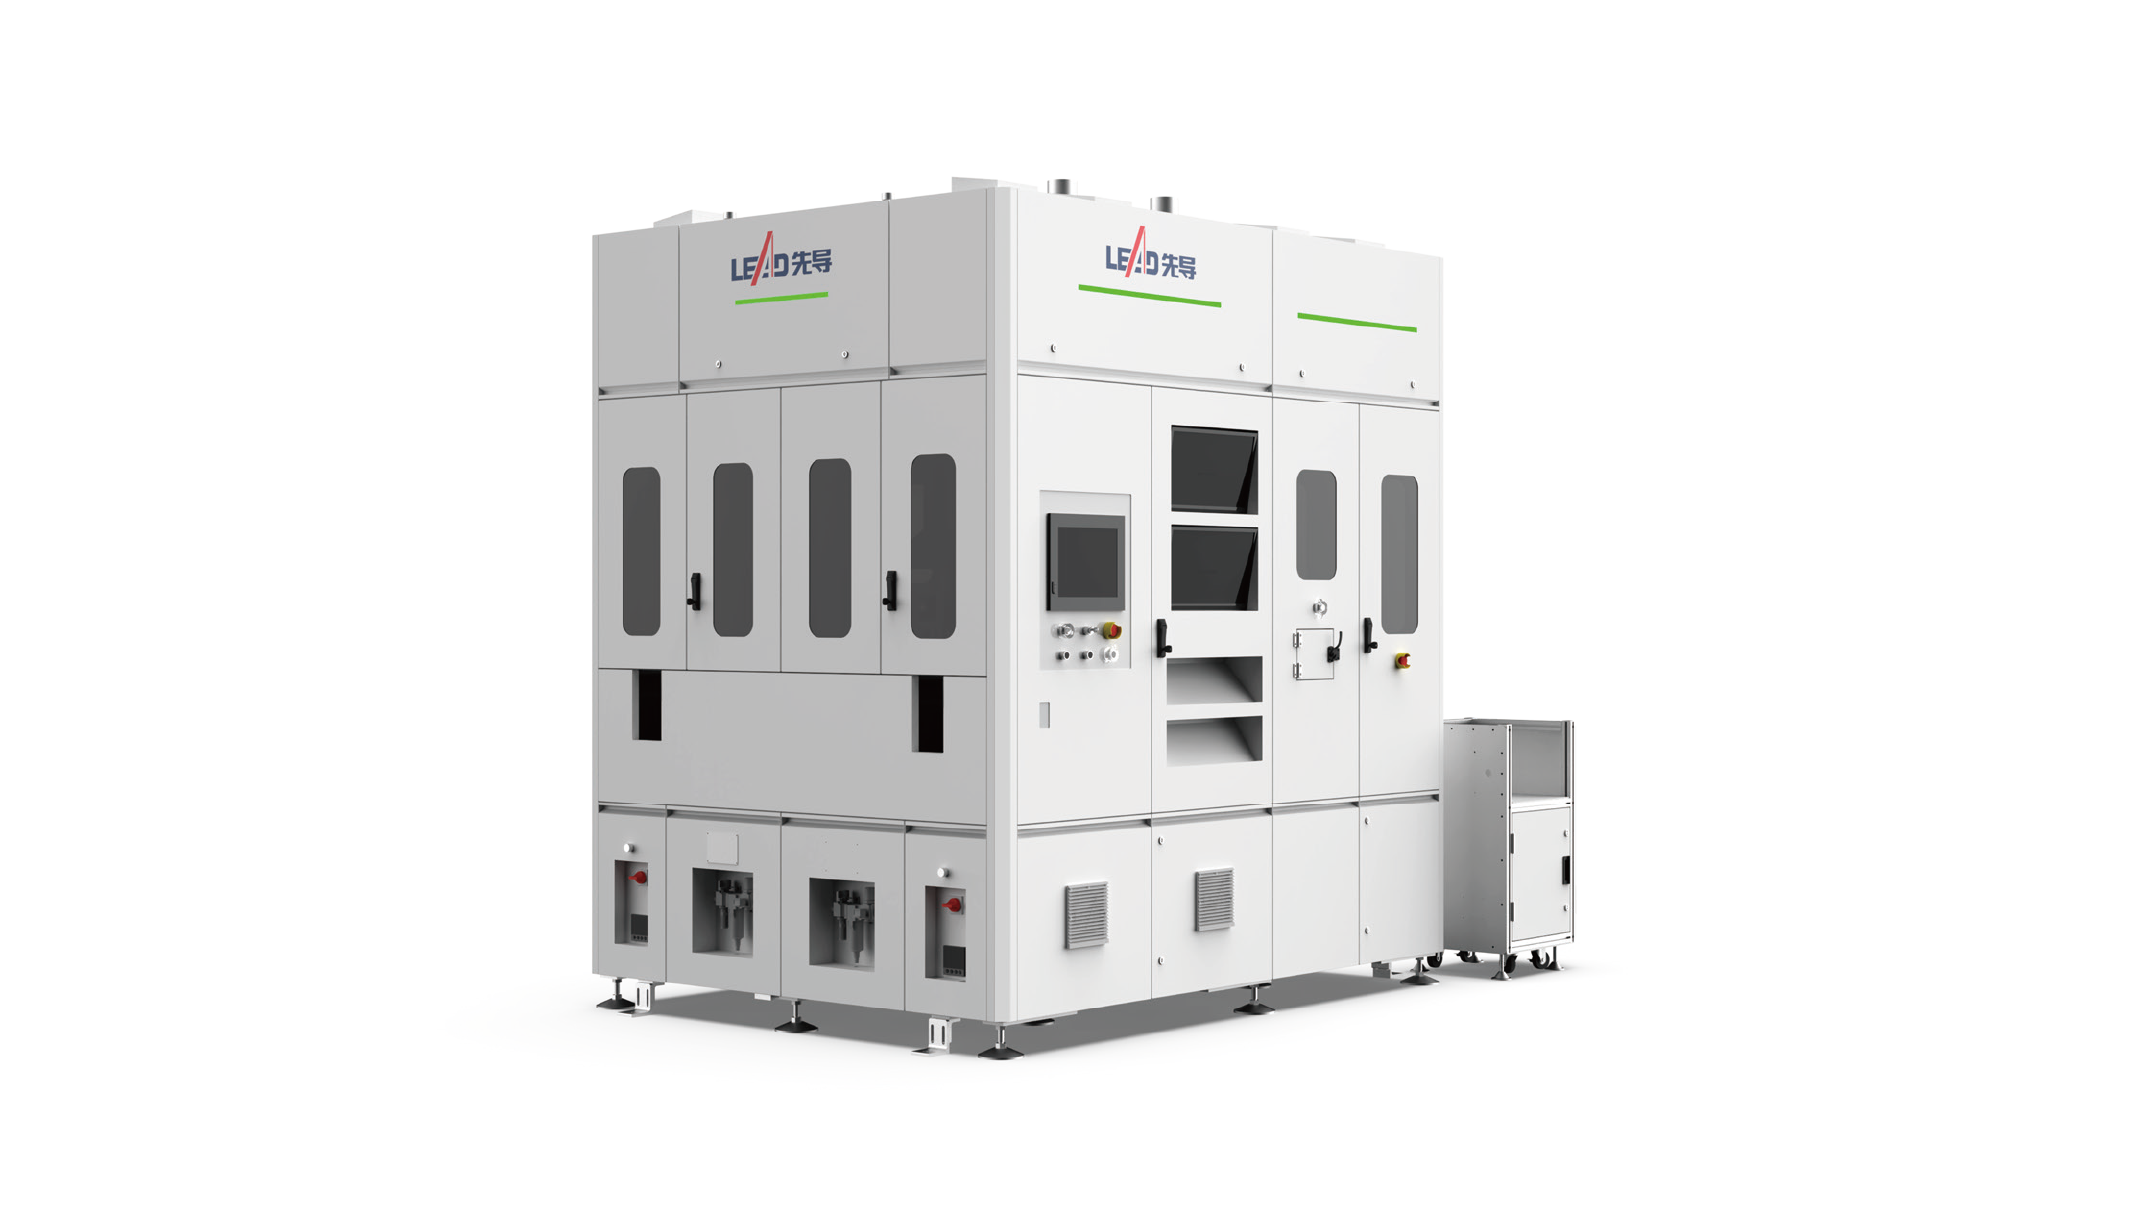
Introduction: Where Speed Meets Scrap Risk
Here’s the truth: speed without control is just expensive waste. In many plants, we push hard to hit weekly targets, but the scrap cart tells a different story. Lithium battery production sits right in this tension, where every minute counts and every defect hurts. Picture a shift change, a rush order, and a small misalign at the welding cell—boom, ten packs on hold. You feel that? Now add the data: OEE drops five points, rework spikes, and delivery windows get tight. So the real question is simple. How do we unlock faster cycle time without trading away quality or pushing operators past their limits?
I’ve seen lines add robots and still stall because the upstream checks are slow. Or the AGVs wait on a clogged station while laser welding is idle—funny how that works, right? The gap is not only hardware. It’s the handshake between steps, the clarity of data, and the control loops that keep drift in check. If we compare lines that win and lines that lag, the difference isn’t magic. It’s the small moves that compound. Let’s head into those details next.
Why ‘Faster’ Fails: Hidden Bottlenecks in Pack Lines
What breaks first?
Traditional upgrades focus on a single station, not the whole flow. A lithium ion battery pack assembly line often speeds up tab welding or screw fastening but keeps old checks and queues. That means more WIP, not more shipped packs. Look, it’s simpler than you think: when vision AOI flags an issue and the MES can’t route the unit to a fast recheck lane, the cell sits. Then EOL testing faces a surge and starts to batch. At that point, SPC becomes a rearview mirror, not a guide. The result is cycle time creep, with quality alarms that show up late.
There’s also a data trust issue. SCADA screens show signals, but they don’t close loops. Operators see “OK,” yet torque drift or laser tab welding heat input is near the edge. Without edge computing nodes to push real-time setpoint tweaks, the fix comes after the defect. Add BMS flashing variation and a slow leak test, and you get a perfect storm. Power converters in test bays run fine, but queue logic is weak, so assets sit idle while one bay is overloaded. This isn’t a lack of tools. It’s a lack of orchestration.
Comparative Shift: Principle-Driven Gains That Stick
What’s Next
So what changes when we compare old-school “speed-ups” to principle-driven design? First, we move from single-station boosts to whole-line control. A digital twin of the lithium ion battery pack assembly line models flow, not just motion. It predicts queues and auto-tunes buffers. Second, we upgrade checks from after-the-fact to in-line. AOI tied to edge computing nodes can adjust pick force, weld pulse, or dispense volume within seconds. Third, we align data with action. MES rules push units to the right rework cell, while SPC trends trigger micro-calibration at the tool—before the next part arrives. Short loops. Fewer surprises.

There’s a case pattern I like: teams add X-ray CT sampling at defined intervals, not for show but to train the AOI algorithms. They add smart fixturing, so EOL stations share load even when one test changes—the schedule flexes in real time. And they tag every sub-pack link to trace torque and temperature, so a bad crimp doesn’t hide. The interesting part is that none of this demands giant capex (not at first). It demands clarity: pick the constraints, wire the data, and close the loop. Then the magic starts to look normal—funny how that works, right? To wrap, here are three practical metrics to judge next steps: 1) percent of defects detected in-station rather than at EOL; 2) average queue time per high-runner station; 3) auto-correction rate from rules pushed by MES or edge logic. Use those, and you’ll see steadier yield and smoother flow. When you need a reference point or partners who’ve done it at scale, there’s always LEAD.