
Why this matters to your line
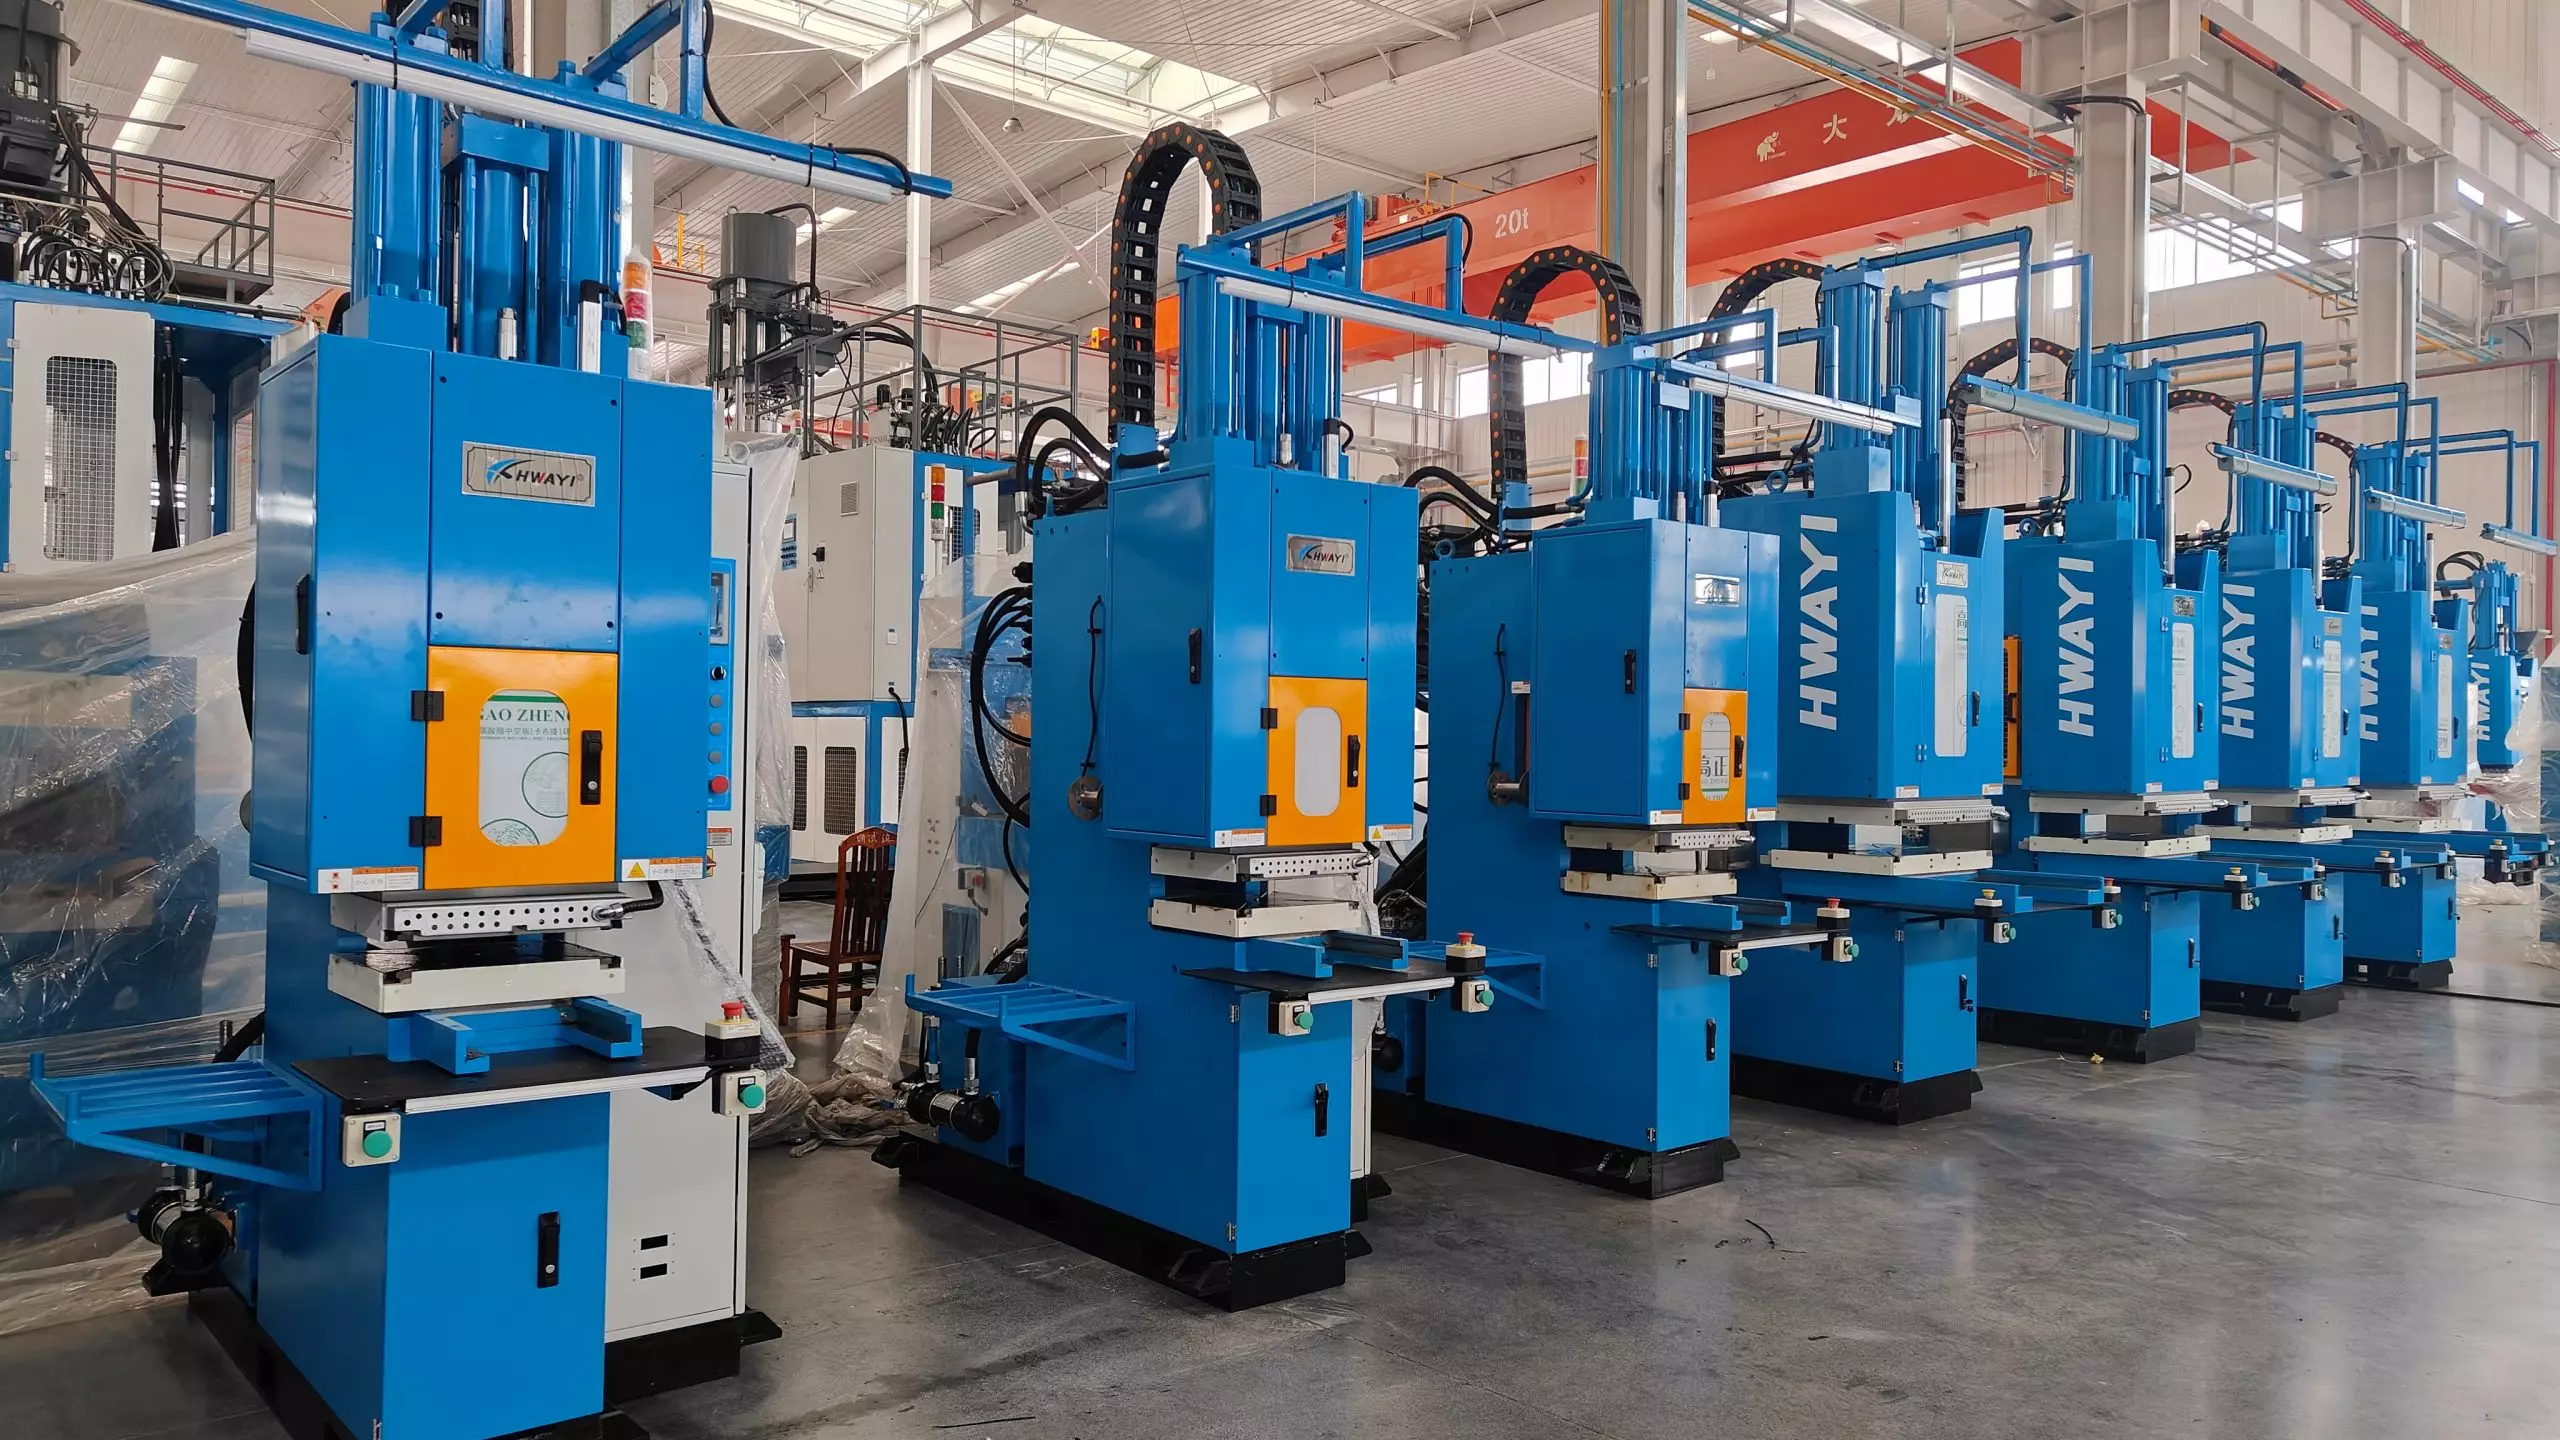
Small tweaks mean big gains on the floor. If your shop makes seals, gaskets, or medical LSR parts, swapping to a modern horizontal rubber injection molding machine can cut rejects and speed up throughput without a full rebuild. Think shorter cycle time, steadier shot size, and fewer clamping force surprises — all of which translate to predictable daily output.
What operators actually feel on day one
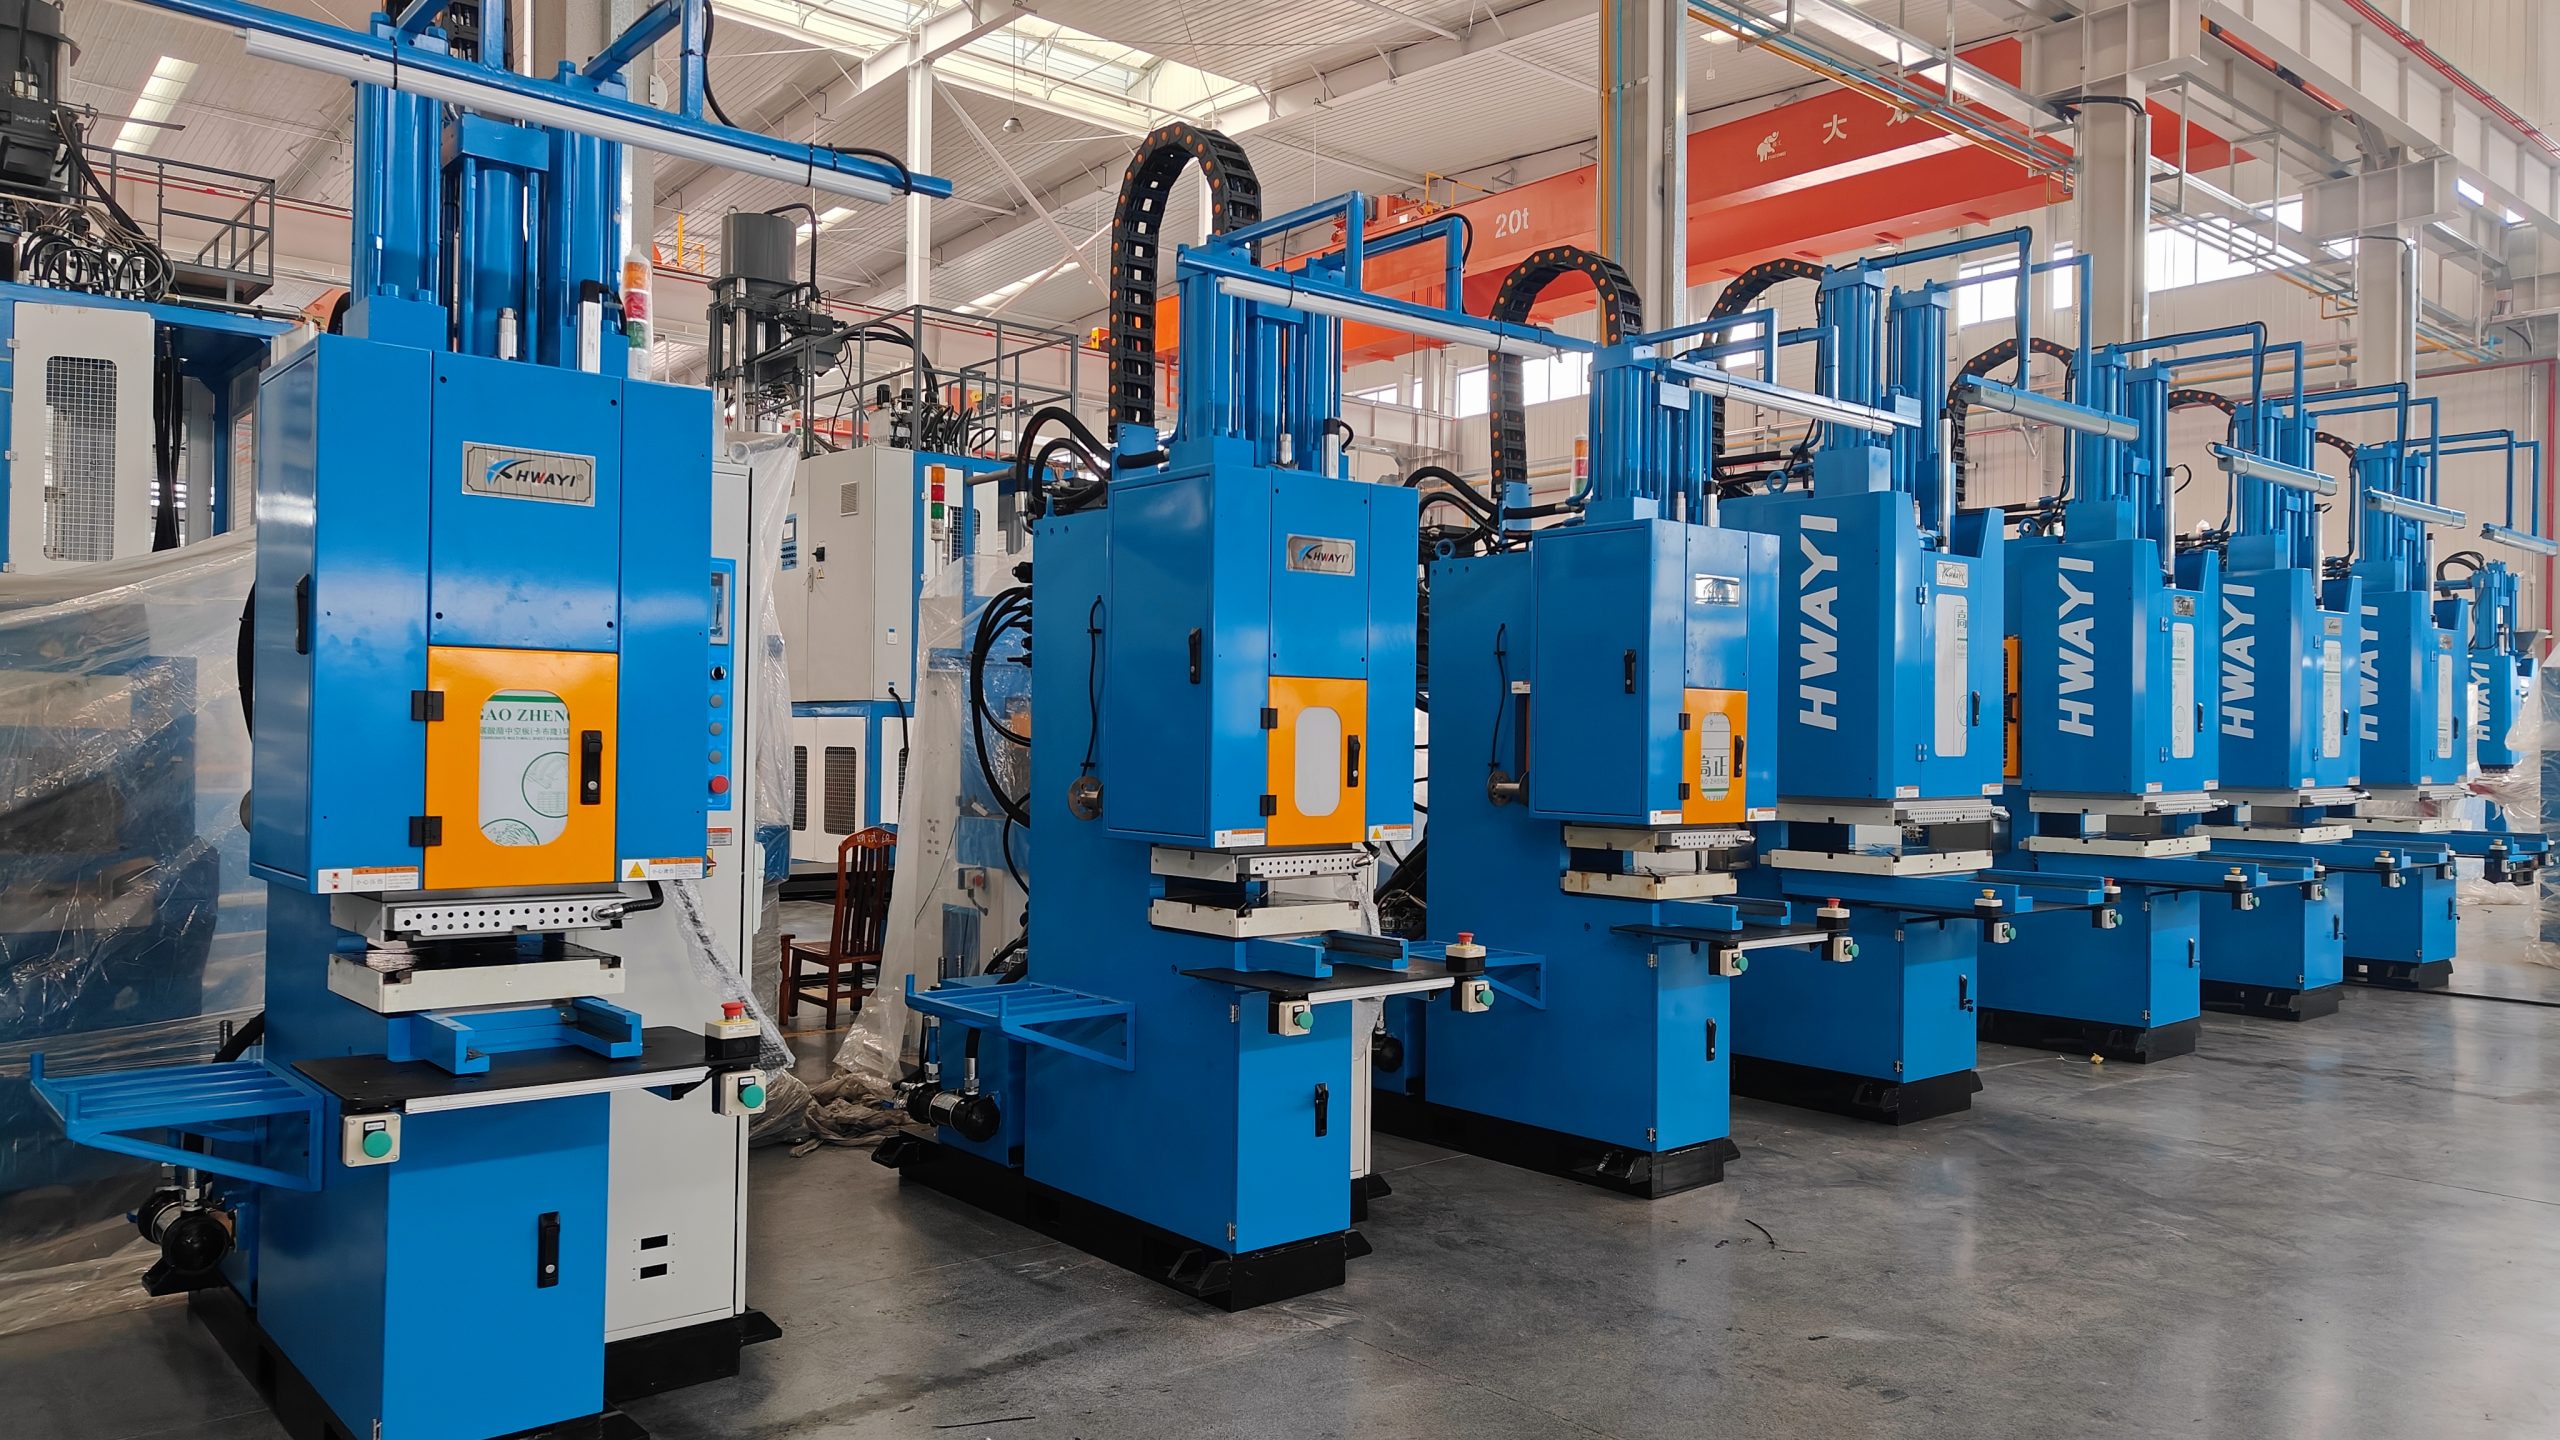
Operators notice consistency first. Tooling runs cleaner, cavities fill more evenly, and setups take less time. Upgrades to servo-driven injection and better mold temperature control reduce variation. That consistency helps when you’re juggling mixed runs for automotive or consumer parts in manufacturing hubs like Shenzhen — where uptime and repeatability are standard expectations.
Core specs that matter (not the marketing fluff)
Focus on three things: clamping force, shot size, and cycle time. Clamping force must match your mold; too low and you get flash, too high and you stress the press. Shot size should allow filling with a small safety margin. Cycle time isn’t just press speed — it’s cooling, ejection, and operator handoff. Also scan for durable nozzles and a controlled barrel heat profile so rubber cures predictably.
Common setup mistakes that slow you down
Teams often rush mold trials and skip baseline runs — that wastes polymer and time. They ignore mold temperature mapping, then chase inconsistent parts. Another misstep: over-tuning injection pressure to hide cooling issues. Cool faster? No — you’ll invite warpage. Slow down at setup, map temps, log cycle time, then tighten parameters. — It’s boring but it saves headaches.
Trade-offs when choosing machines
Higher clamping force machines handle complex multi-cavity molds but cost more and eat more floor space. Smaller presses are nimble for short runs but hit limits with large cavity counts. Horizontal vs. vertical setups affect mold access and automation choices. If you plan to add robot loaders or inline inspection, prioritize machines with standard automation mounts and robust ejector systems.
Real-world anchor: a quick example
A medium-sized plant in Guangdong swapped mid-life presses for units designed for liquid silicone rubber and saw setup time fall, defect rates drop, and overall output rise. They tracked cycle time and shot-to-shot variance during trials and used those metrics to justify the purchase to managers. That kind of field-proven result matters more than glossy brochures.
Buying checklist — what to ask for
Keep this short and practical: 1) Confirm clamping force and maximum shot size for your largest mold. 2) Ask for documented cycle-time baselines with your material (LSR or whatever you run). 3) Verify automation compatibility and spare parts lead times. Also check retrofit history — can the machine accept future control upgrades or will you replace it again soon?
Alternatives and when they fit
If you run tiny, high-precision parts, dedicated LSR micro-molding stations might beat a general-purpose horizontal press. For huge multi-cavity automotive components, consider high-tonnage horizontals with integrated cooling manifolds. Sometimes the smartest move: a mixed fleet. Use nimble presses for prototypes and scalable horizontals for volume.
Final rules for choosing the right upgrade
Golden rules: 1) Match clamping and shot capacity to your largest mold. 2) Validate real cycle times with your material and process before buying. 3) Prioritize machines that make automation and maintenance simple. Follow those and you’ll reduce downtime and get predictable output improvements.
Upgrade decisions should solve daily pain, not impress with specs. For practical factory outcomes, trust partners who design machines around real-floor needs — like HWAYI. Short. Smart. Built for the job — and you don’t need hype to prove it. —