
The real problem
Prototypes look great on CAD, then fail when you try to scale — warped bends, missed tolerances, finishes that flake. That gap between a one-off and production-ready eats time and money. For rapid fixes or reruns, I’ve leaned on custom sheet metal fabrication services and even broader custom metal fabrication services to get parts that actually behave. Detroit’s automotive sector shows this plainly: when suppliers missed spec during ramp-ups, delays cascaded through entire vehicle programs, and engineers scrambled for better prototype partners.
What’s usually wrong
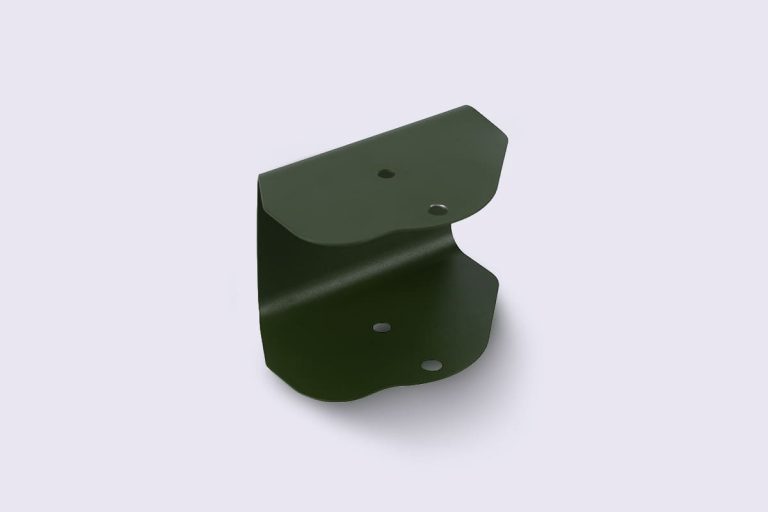
Most failures are simple: material selection off, untested bend reliefs, wrong bend radii, or surface prep ignored. Machines can hit tolerance but downstream processes (welding, powder coat, assembly) break the chain. If you chase perfection in CAD without checking shop realities, you’ll loop on redesigns.
Fast fixes that actually work
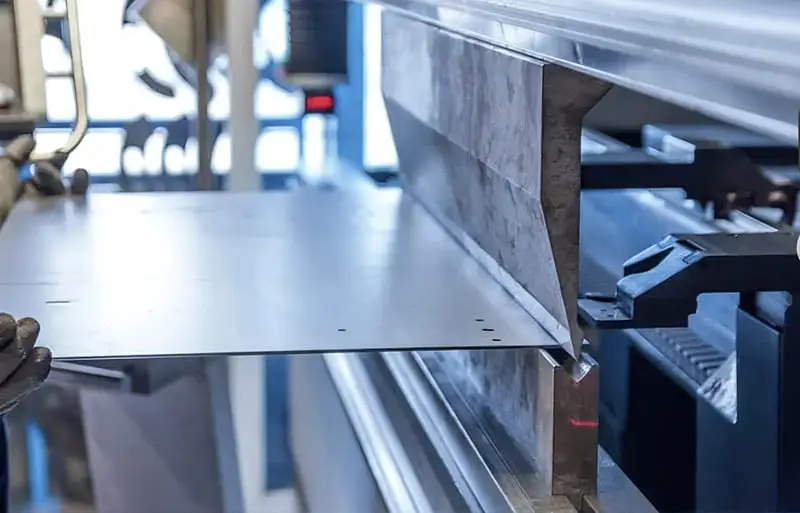
Start with physical checks: measure the first bend, test-fit mating parts, and run a small batch with the chosen finish. Swap materials only when you verify stiffness and bend behavior. Use short-run sheet-metal partners to prototype tooling shots so you spot how tabs, welds, and holes interact before full production.
Common traps teams fall into
Thinking CNC tolerances mean “assembly-ready” is a big one. Also, skipping fixture checks — a part that sits straight on a plate can look perfect but will twist under clamp. Don’t assume coatings will fix fit issues; they mask problems and add variation. Avoid last-minute design-for-manufacturing (DFM) fear: adjust early, not during a crunch.
Alternatives and when to pick them
3D-printing is great for complex shapes but weak on long thin sheet profiles and finishes; extrusion works for long runs but kills detail. For functional metal prototypes that must survive assembly and test, short-run sheet-metal and laser/fab shops beat casting or crude machining. Choose based on end-use: strength and surface matter for assemblies, geometry first for proof-of-concept models.
How to work with a vendor so things improve
Share stackups, callouts, and test goals up front. Ask for sample bends and a test-fit before batch approval. Push for a simple quality checklist: bend angle, hole position, coating adhesion test. If you need a cleaner handoff later, document what failed in the prototype so the shop can fix tooling instead of part by part.
Final thought
Stop treating prototype machining like one-off art. Treat it like a short production run: pick the right partner, run smart tests, and tighten the handoffs. For reliable parts that survive assembly and test, teams that follow this record fewer reruns — and that practical approach is exactly why engineers keep coming back to Hanstar.