
Introduction — a quick scene, some numbers, and the question
I was standing next to a part that had been rejected three times before lunch — tiny burrs, wrong contours, and a frustrated operator tapping the CNC screen. In that same plant, machines from DMG MORI, Mazak, Okuma, Makino, and Haas were all humming away, each promising faster cycle times and tighter tolerances. Recent data shows shops adopting 5-axis cells grow throughput by double digits in under a year; yet many teams still struggle with setup time, tool paths, and long lead approvals (you know the drill). So what makes one 5-axis system actually better for real shop floors, and how do we cut through marketing to pick the right one? Here’s where we start — I’ll walk you through what I’ve seen work and what keeps being a headache for people who run real programs, not just demo rooms.
Deep Dive: Why traditional fixes miss the point
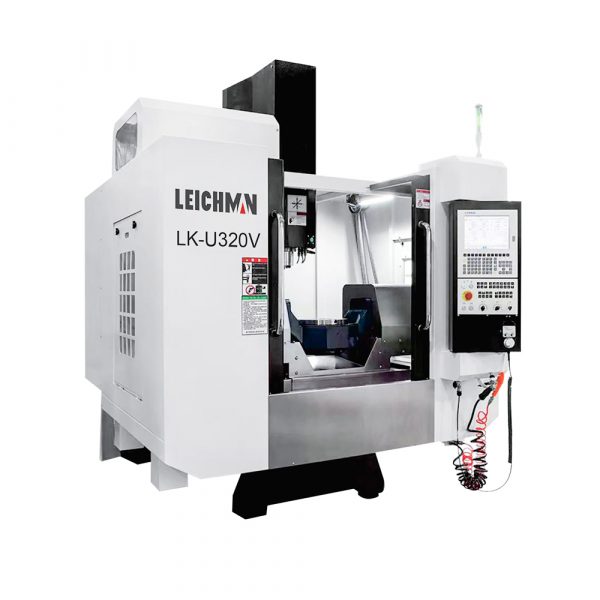
5 axis high speed machining promises speed and finesse, but in practice many shops hit the same snags again and again. From my hands-on time, the classic fixes — more spindle rpm, canned cycles, or thicker coolant flow — only paper over deeper mismatches between software, fixturing, and operator skills. When you push spindle speed and feed rate without matching chatter control and rigid fixturing, the part quality slides. I’m not exaggerating; I’ve reprogrammed jobs mid-shift to stop scrap. Industry terms to keep in mind: spindle speed, tool changer, and servo drives — they matter, but not in isolation. Look, it’s simpler than you think: ramping RPM alone won’t solve interpolation or tool reach problems.
Two technical blind spots stand out. First, CAM toolpath strategies are often designed for ideal geometry, not messy fixtures or bar stock wobble. That mismatch creates workarounds — slower feeds, extra finishing passes. Second, control system limitations (axis coupling and backlash compensation) can blow up a seemingly perfect program. These are not problems you fix with a single upgrade; they require a systems approach: better CAD/CAM integration, tighter torque tuning, and more realistic simulation. I’ve learned to ask one blunt question whenever a vendor promises “faster” — faster than what? The baseline matters. — funny how that works, right?
So what about the user experience?
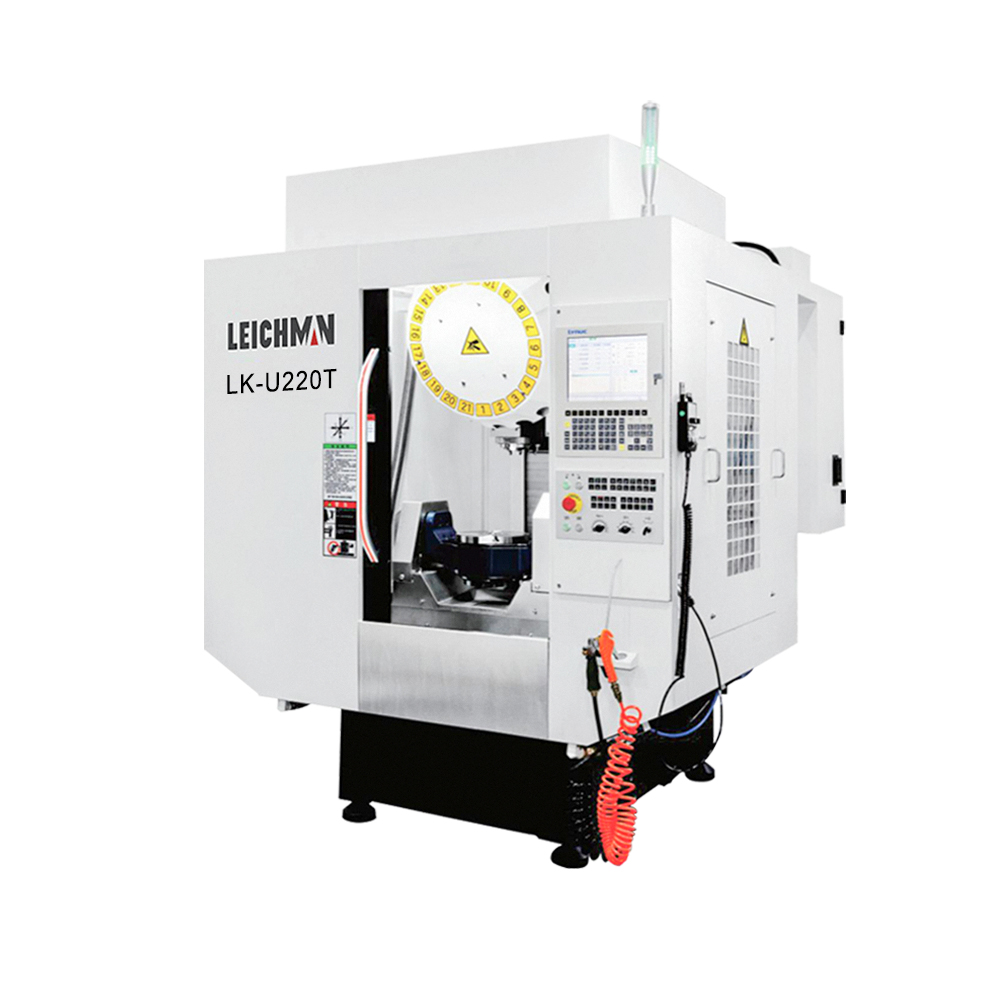
Operators want predictability more than top-end numbers. If the HMI is confusing or tool change alerts are cryptic, cycle time gains evaporate. That human factor keeps coming up in my visits: training, step-by-step tool libraries, and simple fault recovery routines deliver more uptime than flashy specs alone.
Looking Forward: Principles for smarter adoption
When I look ahead, I focus on three new-principle areas that actually change outcomes. First, closed-loop integration between CAM and the controller — not just NC code exports, but native toolpath handoffs that preserve machining intent. Second, adaptive control techniques that tune feed rates on the fly based on spindle load and vibration. Third, modular fixture tooling that reduces setup iterations. These principles shift emphasis from raw spindle speed to consistent, repeatable results. Also, we need to rethink diagnostics: edge computing nodes on the floor can capture spindle torque and axis vibration in real time, letting teams act before a part goes bad. (That’s a lifeline for smaller shops.)
I want to be clear: adopting these ideas takes planning. You’ll need better CAM-post processors, skilled setup people, and sometimes upgraded power converters for stable servo performance. But the payoff is predictable: fewer rework cycles, higher first-pass yield, and less stress for your crew — and yes, more sleep for managers. — and yes, I’ve seen it in action.
What’s next for shops and engineers?
Here are three evaluation metrics I now use when I advise teams choosing a high speed machine: 1) Real-world cycle-time delta — measure a representative part from your shop, not a vendor demo; 2) Integration score — how well does the controller accept CAM toolpaths and process parameters without manual rewriting; 3) Recovery and maintainability — how fast can an operator clear a fault and resume a job. Score each on a simple 1–10 scale and weight them to your priorities.
In short, specs matter, but systems thinking wins. I believe the best purchases come from testing real parts, involving shop floor users, and insisting on measurable metrics. If you want a starting point for tests or a checklist for vendors, I’ll gladly share mine — I’ve built one that saved a mid-sized shop nearly 18% in cycle time within six months. For more product details and a practical place to begin, check out Leichman.